Hey everyone, if you’re deep in the semiconductor game — whether you’re managing a fab floor, sourcing critical process gear, or just trying to wrap your head around why DI water isn’t just “regular old filtered water” — you’ve landed on the right post. I’m [Just our team, we’re the folks building and maintaining deionized water systems for the industry], and let’s cut to the chase: most people outside semiconductors have no clue that the water powering your phone’s chip is way more precise than anything used in a hospital or a fancy coffee shop. Today, we’re breaking down the exact, non-negotiable requirements a semiconductor DI (that’s deionized, for the newbies) water system has to check off. No boring jargon dumps — just real stuff we deal with every day. Deionized Water System
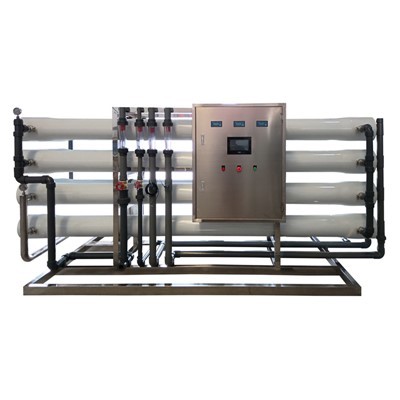
First off, let’s get one myth out right now: DI water for semis isn’t just “no ions.” It’s about zero almost everything else, and the specs? They’re not just made up — they’re tied directly to how a chip gets made. Even a tiny speck or a leftover ion can tank a $10,000 wafer, so the system’s gotta act like a hyper-vigilant gatekeeper 24/7. Let’s start with the big, non-negotiable purity metrics, because these are the backbone of any semi-grade DI system.
Resistivity is the first one everyone talks about, and for good reason. Tap water’s resistivity is like 0.00002 ohm-cm (it’s super conductive because of all the dissolved salts), but semi DI water needs a minimum of 18.2 megohm-cm at 25°C. Wait, that’s not a typo — 18.2. Why? Because any ion (like sodium, chloride, or even heavy metals) messes with the delicate chemical reactions during wafer cleaning and photoresist stripping. Think of it like this: if your water has even a tiny bit of sodium, it’ll leave a residue on the wafer that ruins the next step of laying down tiny circuit patterns. Our systems use mixed-bed ion exchange resins and sometimes electrodeionization (EDI) to nail that resistivity number — no cutting corners here. Even a dip below 18.1 for more than a few seconds is a red flag for us.
Then there’s total organic carbon (TOC). TOC is basically all the dissolved gunk that’s not an ion — things like leftover cleaning chemicals, bacteria byproducts, or even tiny bits of plastic from pipes. For semis, TOC has to be below 1 part per billion (ppb), and some advanced nodes (the 3nm, 5nm stuff everyone’s hyped about) even need it below 0.5 ppb. Why care? Because organic compounds break down into smaller particles that can stick to wafers, or react with the photoresist used to print circuits. We add ultra-violet (UV) oxidation units to our systems — these blast the water with deep UV light that breaks down organic gunk into carbon dioxide and water, so we can filter it out. If you skip the UV, your TOC will creep up before you know it, and fab guys will be calling at 2 a.m. about a bad batch.
Particulates are another beast. Particles in water can scratch the wafer, clog tiny valves, or get trapped between circuit layers. For semis, we’re talking particles as small as 0.05 micrometers — that’s way smaller than a red blood cell. The system’s particulate count has to be less than 10 particles per liter of water for 0.05μm particles, and almost zero for anything bigger. We use a series of membrane filters, starting with 0.2μm filters and moving up to ultrafiltration (UF) for the really tiny stuff. And we don’t just install filters and walk away — we monitor them nonstop, because even a tiny tear in a filter element can let a flood of particles through, and that’s a fab’s worst nightmare.
Wait, we can’t forget about microbes, either. Bacteria and other microbes love hanging out in water systems, and their tiny cells are a form of particulate that can mess up wafers. For semiconductor DI water, microbial count has to be below 1 colony-forming unit per milliliter (CFU/mL). We tackle this with a combination of UV disinfection, periodic chemical sanitization, and even biocide treatment (but super controlled, because too much biocide can leave its own residue). A lot of smaller systems skip the continuous monitoring for microbes, but here’s the thing: microbes can multiply fast, so if you’re not checking, you’ll only find out when your wafer yield drops. That’s why we add real-time microbial sensors to our designs — it’s not overkill, it’s required.
Now, it’s not just about what gets removed — it’s about how the system works day in and day out. Semiconductor fabs run 24/7, 365 days a year. If your DI water system goes down, the entire fab might shut down, and that’s millions of dollars in lost production every hour. So reliability is a huge requirement. Our systems are designed with redundancy — critical parts like pumps, filters, and even the EDI units have backup. We also use materials that don’t leach anything into the water. Normal PVC pipes might leach plasticizers, so we use high-purity polyvinylidene fluoride (PVDF) or perfluoroalkoxy alkane (PFA) piping. That’s non-negotiable. If your pipe leaches, you’re defeating all the purity work you did with filtration and resins.
Then there’s monitoring and control. You can’t just set up a DI system and forget it. You need real-time data on resistivity, TOC, particulates, microbial count, and flow rate. Most fabs use SCADA systems, and we build our DI systems to integrate seamlessly with that — so fab engineers can check everything from their control room, no matter where they are. We also add alarms that ping our team 24/7 if something’s off, like a resistivity drop or a filter pressure spike. That means if a part starts to fail, we can fix it before it causes a problem. Trust me, we’ve been in the game long enough to know that the best way to avoid a 2 a.m. call is to catch issues before they happen.
Wait, there’s also the matter of water stability. When DI water sits still, it can absorb carbon dioxide from the air, which lowers the resistivity over time. So our systems have closed-loop recirculation. The water doesn’t just sit in a tank — it’s pumped through the system constantly, so it doesn’t have time to pick up CO2 or contaminants. We also keep the system pressurized, which prevents air from getting in. That’s a small detail, but it makes a huge difference in keeping that 18.2 megohm-cm resistivity consistent.
Oh, and let’s talk about specific ion contaminants. We’ve mentioned sodium, but there are plenty of other ions that are bad news for semis: potassium, calcium, magnesium, chloride, sulfate, and even heavy metals like lead or arsenic. All of these have to be below parts per trillion (ppt) levels for advanced nodes. Mixed-bed ion exchange resins are key here, because they can grab almost every type of ion. We also use reverse osmosis (RO) as a pre-treatment step before the EDI and mixed beds — RO removes 99% of the initial ions from the feed water, which makes the rest of the purification easier and more efficient. If your feed water is extra contaminated (like if a fab is in a place with hard tap water), we might add a softener or another pre-treatment step to protect the more expensive purification parts.
Now, here’s something a lot of people don’t think about: scalability. Semiconductor fabs grow, and their water needs grow with them. A good DI system has to be designed so you can add capacity without replacing the whole thing. We build our systems with modular parts, so if a fab needs more water in a year or two, we can just add another EDI unit or another set of filters instead of starting over. That saves fabs a ton of money, and it’s a requirement for long-term partnerships.
Wait, let’s get real about the mistakes we see sometimes. A few years back, we worked with a new fab that tried to cut corners on UV oxidation for TOC. Their TOC crept up to 5 ppb, and they had a whole batch of 7nm wafers that had to be scrapped — that cost them over $2 million. Ouch. Another time, a different fab used cheap PVC pipes, and the plasticizers leached into the water, causing photoresist adhesion issues. They had to flush the whole system for weeks, which shut down part of their production. That’s why we never cut corners on materials or core components. For semi DI systems, “good enough” isn’t a thing — it has to be exactly right, every single time.
So let’s wrap this up with what all this boils down to: a semiconductor-grade DI water system isn’t just a water filter. It’s a precision instrument, designed to deliver water so pure it’s almost “dead” (in terms of impurities), reliable enough to run nonstop, and monitored so closely that you’ll know if something’s off before it causes a problem. The requirements are specific, they’re non-negotiable, and if you miss even one, you’re looking at wasted wafers, lost production, and big headaches.
If you’re running a fab, or sourcing a DI system for an upcoming project, we’ve built these systems for years — we know the ins and outs, the little details that make all the difference, and how to keep your water specs on point, 24/7. We don’t do one-size-fits-all, either — every fab has different needs, whether they’re making 28nm chips for microcontrollers or 3nm logic chips for smartphones. We’ll work with you to design a system that fits your exact process, your budget, and your long-term goals.
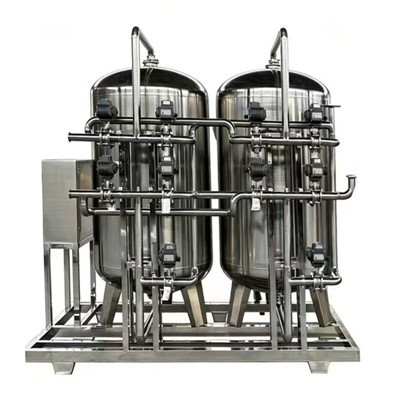
If you’re ready to stop dealing with water-related yield issues or unreliable systems, get in touch with our team to talk through your needs. We’re here to make sure your water doesn’t hold your chips back.
RO Purified Water Equipment References:
- Semiconductor Equipment and Materials International (SEMI). SEMI F63-1102: Standard Guide for Purified Water and Deionized Water for Semiconductor Processing.
- American Society for Testing and Materials (ASTM). ASTM D5127-20: Standard Specification for Ultra-Pure Water Used in the Electronics and Semiconductor Industries.
- International Organization for Standardization (ISO). ISO 3696: Water for analytical laboratory use — Specification and test methods.
- Zhang, L., et al. (2021). “Critical Water Purity Requirements for Advanced Semiconductor Manufacturing Nodes.” Journal of Semiconductor Manufacturing Technology.
Shandong Yanuo Environmental Protection Equipment Co., Ltd.
We’re well-known as one of the leading deionized water system manufacturers and suppliers in China, featured by quality products and good price. Please rest assured to buy bulk deionized water system made in China here from our factory. Customized orders are welcome.
Address: North Side of the Road, 1,000 Meters West of the Intersection of Fenghuangshan West Road and Provincial Highway S102, Wangfu Subdistrict, Qingzhou City, Weifang City, Shandong Province.
E-mail: ynhb.499973983@gmail.com
WebSite: https://www.zkyaruo.com/
